Hey everyone, Line Boring
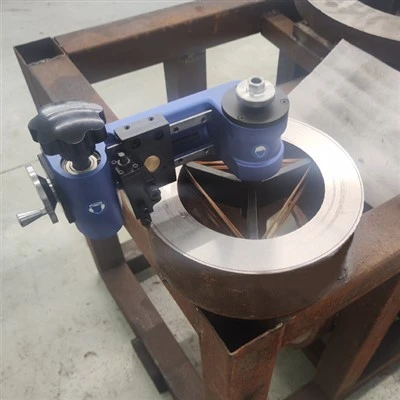
If you’ve ever worked with heavy machinery—think excavators, mining trucks, or big rigs—you know those massive engines and frames have a weird, wobbly way of throwing a fit when something’s even slightly off. And as your go-to line boring supplier, I get more questions than you’d expect about how we actually make sure those bores are dead-on accurate. Like, it’s not just “eyeball it and cross your fingers” (though I’ll admit, I’ve seen some sketchy old-school guys try that back in the day). Let me break this down straight—no jargon, no fancy fluff, just the real way we measure line boring accuracy.
First off, let’s make sure we’re on the same page: line boring is when we bore a straight, precise hole through multiple parts of a machine’s frame or engine to align things like crankshafts, camshafts, or axle pins. If that hole’s even a hair off, you’re looking at vibrations, breakdowns, or worse—you guessed it, a total engine tear-down. So accuracy here isn’t just a “nice to have” – it’s the whole reason we’re in business.
Let’s start with the basics that everyone should know, even if you’re not a line boring tech. The first big check we do is the concentricity test. Wait, what’s that? Basically, it’s making sure all the bores we cut are centered on the exact same imaginary line. If one bore is off by even 0.005 inches, that’s enough to throw a crankshaft out of whack. How do we measure that? We use dial indicators—you know, those little gauge things with a needle that moves when you touch it to something. We clamp a test bar through all the bores, mount the dial indicator on a stand that slides along the bar, and then run it the entire length. If the needle moves more than our tolerance (usually 0.002 inches for most heavy equipment), we’ve got a problem. I’ve had jobs where the frame was bent so bad, we had to re-bore three times before the dial indicator stopped wiggling. It’s tedious, but it’s non-negotiable.
Next up, straightness. Because even if all bores are concentric, if the whole line is curved, that’s just as bad. For this, we use laser alignment tools now, thank goodness—way better than the old string and plumb bob method (don’t even get me started on how windy days ruined those). A laser projector shoots a tiny, precise beam along the path we want the bore to be. We then place targets in each bore, and a sensor measures how far off each target is from the laser. Modern lasers are accurate to 0.001 inches over 10 feet, which is perfect for most line boring jobs. I remember when we still used those old optical levels—you’d spend an hour setting it up, and a gust of wind would shift it, making you start over. Lasers cut that time in half, and the accuracy is way more reliable.
But here’s the thing: measurements don’t mean squat if we don’t account for heat. Heavy steel frames expand when they’re worked on, right? If we measure the bore when it’s cold, then later when the machine’s running, the heat from the engine will make the metal expand, throwing the accuracy off. So we always let the parts cool down to room temperature before taking final measurements. I once skipped that step on a job for a mining company—cut corners, got the bores measured perfect when they were cool, then two weeks later they called saying the engine was vibrating so bad, they had to shut it down. Turned out the engine heat expanded the frame, shifting the bores. Now we have a strict rule: wait at least 24 hours after machining before final checks. Lesson learned the hard way.
Another key measurement is surface finish. Wait, surface finish? Yeah, because even if the bore is the right size and straight, if the inside is rough, the bearings won’t seat properly, and you’ll get wear way faster. We use a surface roughness tester—kind of like a tiny stylus that drags along the bore and measures how bumpy the surface is. For most line boring jobs, we aim for a roughness of 16 to 32 microinches. Too rough, and bearings scrape; too smooth, and they don’t hold lubrication. It’s a sweet spot, and we don’t cut corners here either. I’ve had a client refuse to pay once because our surface finish was 35 microinches—they said their bearings wore out in 6 months instead of a year. We re-did the bore for free, and they’ve been a repeat client ever since. That’s how important that measurement is.
Now, let’s talk about tolerance stacking. If you’re boring multiple bores in a single frame, each bore has its own tolerance, and if they all add up wrong, you get issues. For example, if each bore is allowed to be 0.001 inches off, and you have 5 bores, that’s a total of 0.005 inches of possible error—way more than the 0.002 we’re okay with. So we measure each individual bore’s size first, then how they align with each other, then the total straightness. We write all these numbers down in a job log—no exceptions. Every single measurement, every single check, gets logged. That way, if something goes wrong later, we can go back and see exactly what was done. It’s saved us more than once when a client says “your line boring was off” and we can show them the measurements proving it was perfect.
Wait, and for portable line boring jobs—you know, when we can’t move the machine to the shop, and we have to work on-site? That’s when accuracy gets tricky, because we’re dealing with the whole machine being in place, not just parts on a workbench. For on-site jobs, we use a combination of the laser alignment and the dial indicator test bar, but we also use a coordinate measuring machine (CMM) for final checks. The CMM has a probe that can touch multiple points on the bore and give us exact coordinates, so we can map the entire line. I did a job last year on a big mining dump truck that had a bent frame from tipping. We did line boring on the rear axle, and the CMM confirmed the bore was straight within 0.001 inches. The client said it was the first time their truck didn’t vibrate at 50 mph—game changer.
Now, let’s be real—no measurement is perfect. Even our best tools have a margin of error, usually around 0.0005 inches. That’s why we always do multiple checks. We’ll run the dial indicator test bar twice, check the laser alignment from two different directions, test surface finish in three different spots along the bore. Consistency is key. If all the measurements come out the same, that’s when we sign off on the job. If there’s a discrepancy, we dig into it. Maybe the test bar was bent, maybe the laser was knocked, maybe the frame had shifted when we clamped it down. We don’t leave until every single measurement is consistent and within our tolerance.
As a line boring supplier, this is what I stand for. It’s not just about cutting a hole—it’s about making sure that hole works for you, day in and day out, no breakdowns, no extra costs, no headaches. We’ve been doing this for years, and we’ve fixed everything from small excavators to massive mining equipment. If you’ve got a machine that needs line boring, and you’re tired of dealing with guys who just “wing it” and charge you for it, hit us up. We’ll walk you through the whole process, show you our measurements, and make sure the job’s done right the first time.

Don’t let a bad line boring job ruin your equipment. Let’s get it done accurate, done fast, and done right. Reach out whenever you’re ready to chat about your next project.
Line Boring Bar References
- Machine Shop Practice: Line Boring and Alignment Techniques, 2021, Industrial Press
- Heavy Equipment Maintenance and Repair Handbook, 5th Edition, 2019, McGraw-Hill
- Laser Alignment Systems for Precision Machining, 2022, Society of Manufacturing Engineers
- Surface Roughness Measurement Methods for Machined Bores, 2020, Journal of Machining Science and Technology
Shangqiu JDA Machinery Technology Co., Ltd.
With abundant experience, we are one of the most professional line boring manufacturers and suppliers in China. We warmly welcome you to buy cheap line boring for sale here from our factory. Quality products and reasonable price are available.
Address: No. 55 Pingyuan Middle Road, Liangyuan District, Shangqiu, Henan, China
E-mail: sales@jdamachines.com
WebSite: https://www.jdamachines.com/
